
Blog
Optical injection moulding: precision for lenses, light guides and covers
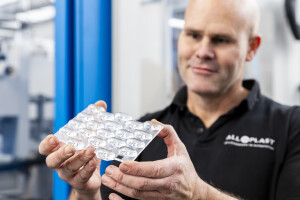
Injection moulding of optical components requires a level of precision, cleanliness and process control that far exceeds that of standard injection moulding. But this also opens up exceptional possibilities.
The specific requirements of optical injection-moulded parts
An optically injection-moulded component is not merely a transparent part. It is a functional optical element in which geometry, surface accuracy and material purity directly determine its optical performance. A lens surface with a micro-irregularity of just a few micrometres can already lead to stray light or image distortion. The tolerances on an optical component are therefore an order of magnitude tighter than in standard injection moulding. Furthermore, the requirements for material purity and processing are much stricter: inclusions, bubbles or birefringence (double refraction caused by internal stress) are all unacceptable.
Lenses and light guides: what makes each type unique?
Optical lenses, such as Fresnel lenses, collimator lenses or spherical lenses for LED lighting, require precise reproducibility of the lens surface. Light guides have different requirements: here, the internal homogeneity of the material is crucial, as is the accuracy of the input and output geometry.
Reflective covers and protective lenses require a uniform wall thickness and a mirror-finish surface. Each type of optical component therefore requires a specific approach to mould design, material specification and process control. There is no one-size-fits-all solution.
Collimator lenses: precise lens geometry for focused light beams
Fresnel lenses: thin-walled, with a complex surface structure
Light guides: homogeneous material, precise inlet geometry
Covers and diffusers: uniform wall thickness, controlled light diffusion
Moulding technology for optical precision
Moulds for optical components are manufactured to a standard of precision far exceeding that of standard mould-making. Lens surfaces are machined on ultra-precision milling machines or EDM machines and then polished to a surface roughness of Ra 0.005 µm or better; a fraction of what is typical in standard optical injection moulding. The cooling system is designed to ensure uniform temperature distribution across the entire lens surface in order to minimise thermal deformation and uneven shrinkage. The mould is manufactured from special steel with a fine, homogeneous microstructure to allow for post-use polishing.
Quality control and validation of optical performance
Quality control of optical injection-moulded components goes beyond mere dimensional inspection. Optical performance is measured using specialised equipment: interferometers for surface shape errors, goniophotometers for light distribution and Tyndall meters for measuring material inclusions. The validation procedure usually also includes functional tests in the end application: the light pattern of a luminaire or the image quality of a camera lens. Only when the functional optical performance also meets the requirements is the mould approved for series production.
At De Beer Plastics, we produce several million optical components every year, ranging from simple to highly complex. The specialised moulds required for this are developed and built in-house.

Moulding challenges into Reality
